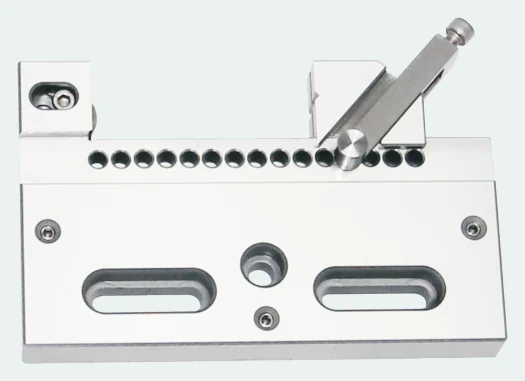
VIS650 Manual Magnetic Vise
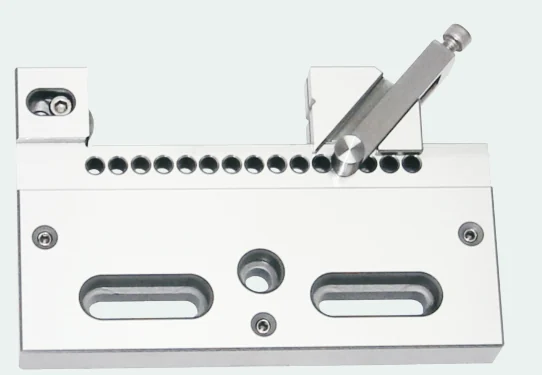
VIS650.75 / VIS650.100Magnetic holding in a compact single body. The hold-down feature prevents the workpiece from lifting during the cut.
A complete, standardised range of EDM vises, bridges, tooling and work platforms — engineered so that every fixture on your machine speaks the same language. Fast to set, precise to hold, effective in production.
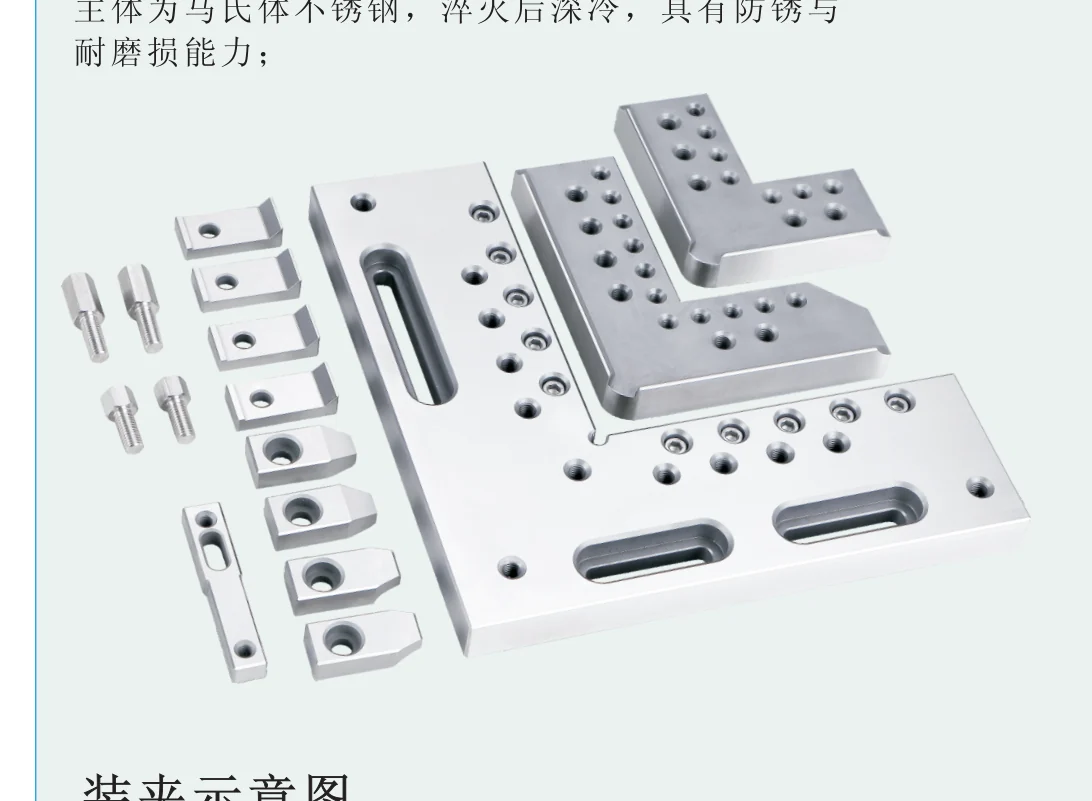
Every family shares the same mounting logic, the same material grades and the same hold-down principle — so a shop can standardise its cell without re-learning every station.
Manual, power-driven, ultra-thin, right-angle and vertical-clamping models.
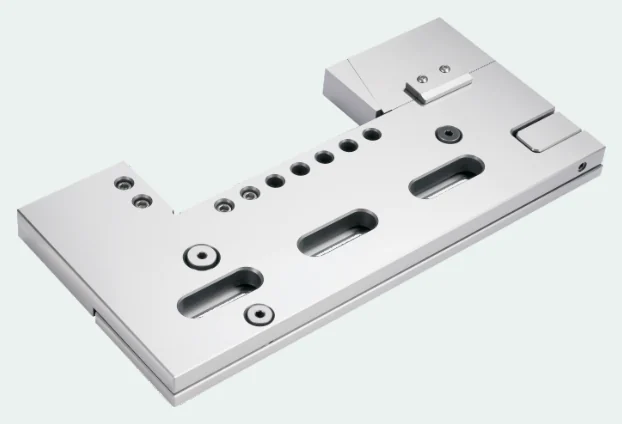
Horizontal, vertical and parallel adjustment for fast setup without rework.
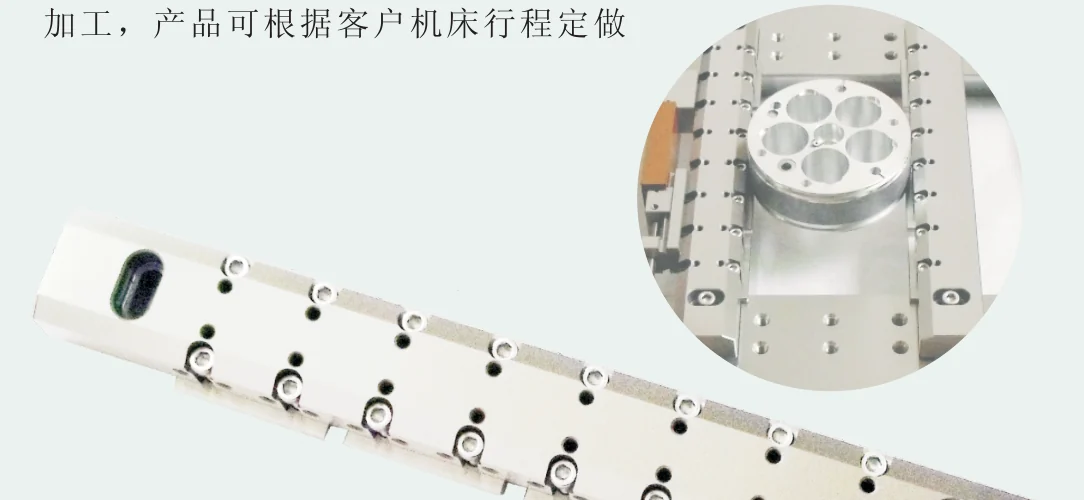
Modular bridge fixturing for large workpieces and extended work stands.
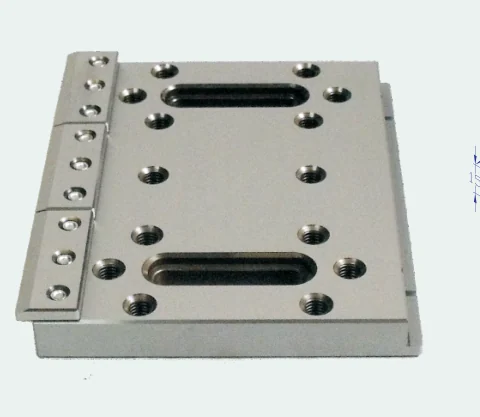
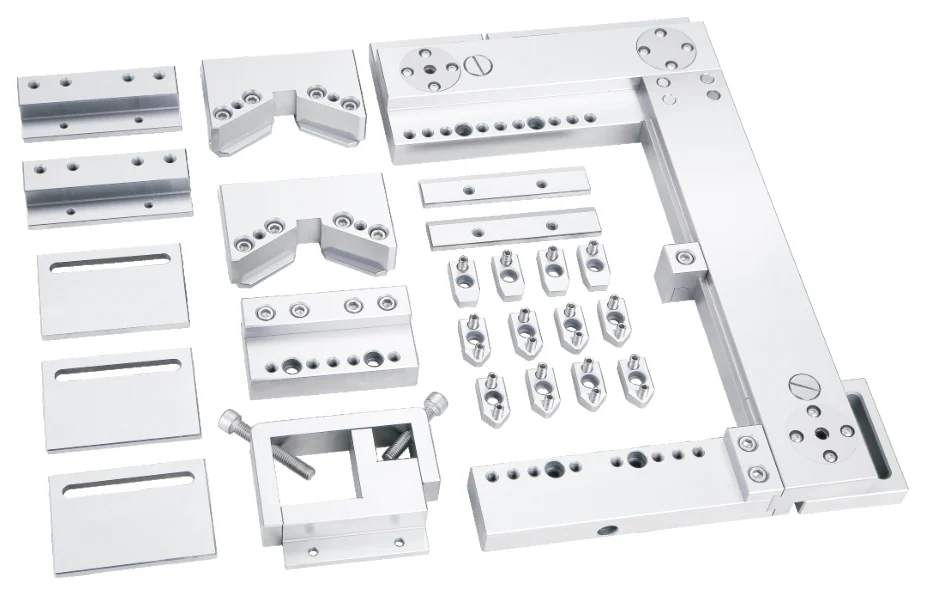
One-eye, two-eye, three-eye, angle tooling, extensions and hold-down plates.
On a wire-cut EDM the workpiece is held on a thin, floating table and the wire must never touch the fixture. These constraints drive every feature in the range.
A positive downward hold-down keeps the workpiece seated, so thermal expansion during a long cut can never raise it off the table.
Clamping is directed downward and forward at 45°, so the workpiece is pressed firmly against the table rather than pushed sideways.
Machined from one solid body where possible — fewer interfaces mean better parallelism and far less deflection under clamping load.
Bridges, vises and tooling share one hole grid, so a fixture built for one station can be reconfigured for the next job.
Aluminium bodies for lightness, SUS440 / HRC 50–55 maraging steel where wear matters — flatness and squareness held to 0.005 mm per 100 mm.
Screw-holder lock structures and single-lever clamping mean a new job can be fixtured in minutes, not an afternoon.
Six models that cover the majority of daily wire-cut fixturing work.
Magnetic holding in a compact single body. The hold-down feature prevents the workpiece from lifting during the cut.
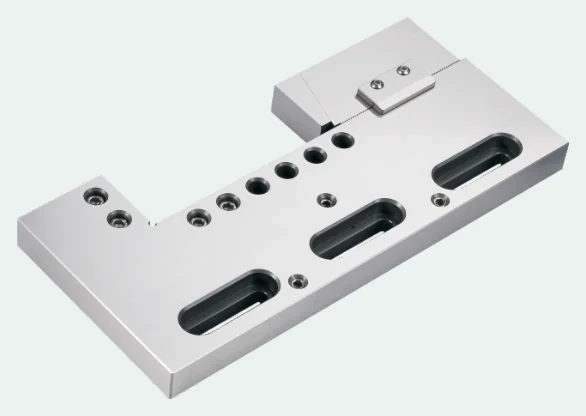
Clamping force applied at 45° obliquely downward. Compact size suits small workpieces; holds up to 12 kg.
Horizontal, vertical and parallel adjustment in one body. Attach to the work stand once, then re-centre in seconds.
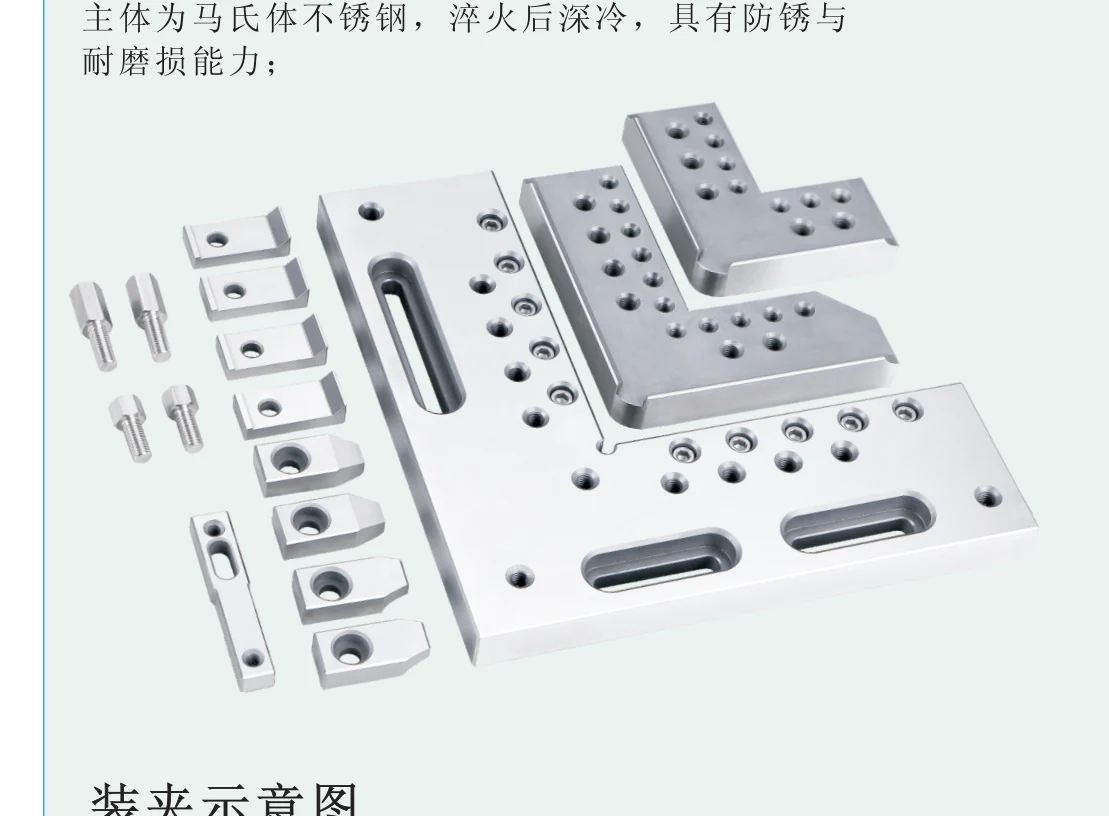
A full kit of right-angle clamping faces and blocks. A single set covers square, stepped and profiled work.
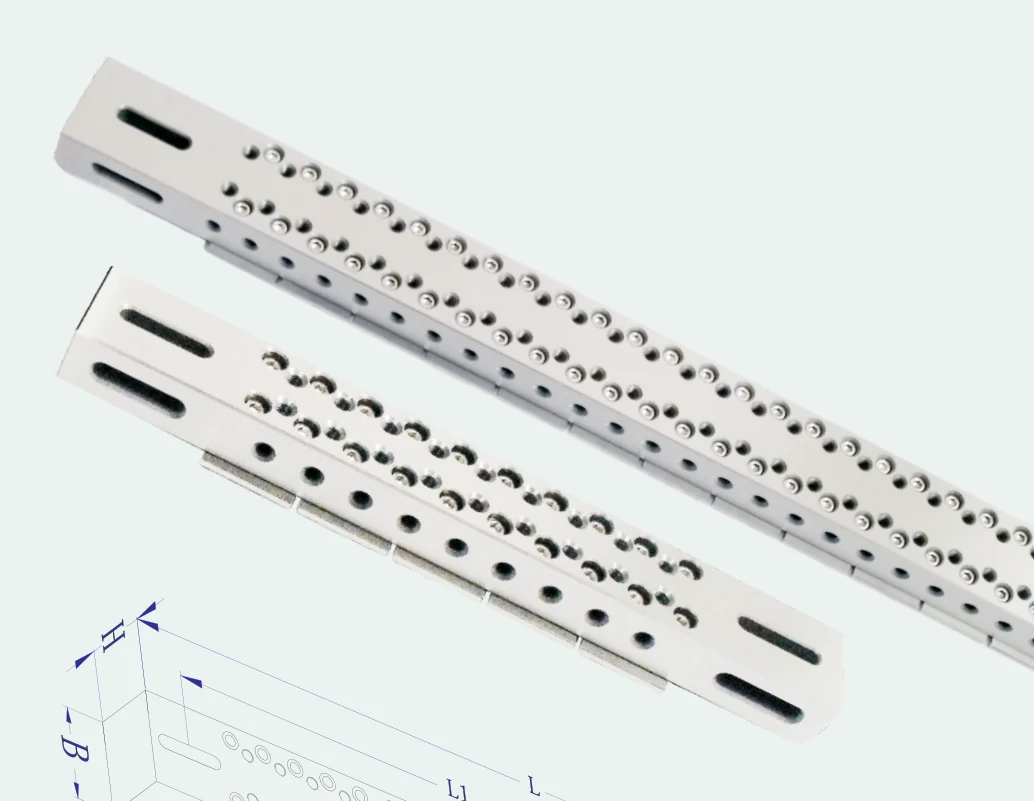
Maraging stainless steel bridge for large workpieces, sized to the centre distance of your machine table.
The horizontal centring backbone of the system — special bearings let you centre a workpiece quickly and accurately.
An EDM fixture lives a hard life: constant thermal cycling, water-based dielectric, and a workpiece that is being eroded a few millimetres away from it. Material selection matters more here than in ordinary machining.
| Property | Specification |
|---|---|
| Material (bridge) | SUS440 maraging steel |
| Hardness | HRC 50–55 |
| Flatness | 0.005 mm / 100 mm |
| Parallelism | 0.005 mm / 100 mm |
| Squareness | 0.005 mm / 100 mm |
| Wire clearance | 0.2 mm leeway after adjustment |
| Clamp capacity | up to 20 kg (tooling series) |
Machine model, table centre distance, workpiece material and the drawing of your part.
We propose the vise or bridge combination, with clamping force and capacity checked against your cut.
Machined, ground and inspected. Tolerance reports issued with every custom assembly.
Existing fixtures are repaired, re-bored or adapted as your machine and parts change.
Send your machine model and a drawing or photo of the workpiece. We will recommend a model and quote from the standard range — or propose a modification if the standard part falls short.